How to Calculate Concrete Block Machine Production Capacity

09.09.2026

One of the first questions investors ask when evaluating a concrete block machine is:

“How many blocks can this machine produce per day?”

The question appears simple, but a reliable answer requires more than reading a capacity figure from a machine catalogue.

Concrete block machine output depends on several variables, including:

  • Cycle time
  • Number of mould cavities
  • Product dimensions
  • Production pallet size
  • Concrete feeding time
  • Vibration and compaction time
  • Mould-changing time
  • Shift efficiency
  • Reject rate
  • Batching and mixer capacity
  • Curing capacity
  • Packaging capacity

This means there is an important difference between:

Theoretical machine capacity

and

Actual saleable production capacity.

Theoretical capacity assumes that the machine operates continuously under ideal conditions.

Real production includes cleaning, maintenance, material changes, mould changes, operator interventions, quality checks and unexpected interruptions.

For an investor preparing a feasibility study, the second figure is much more important.

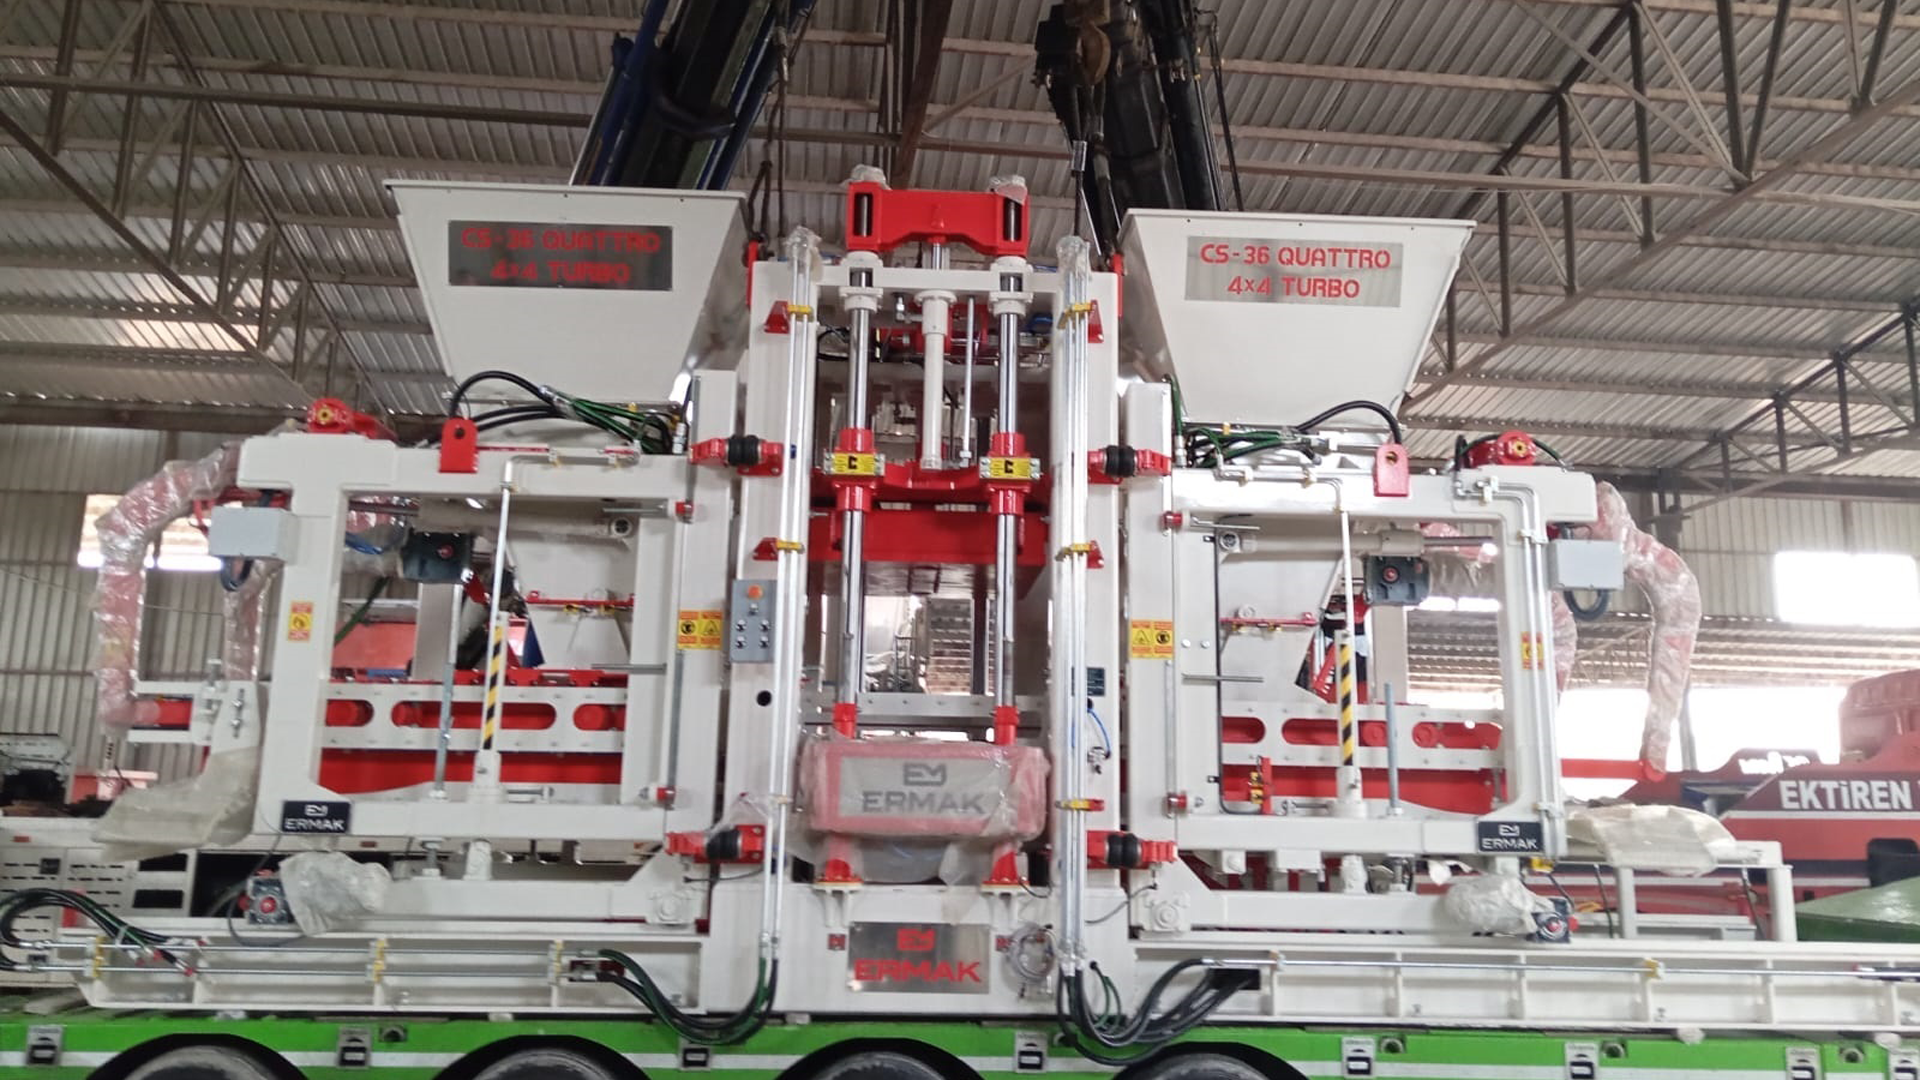
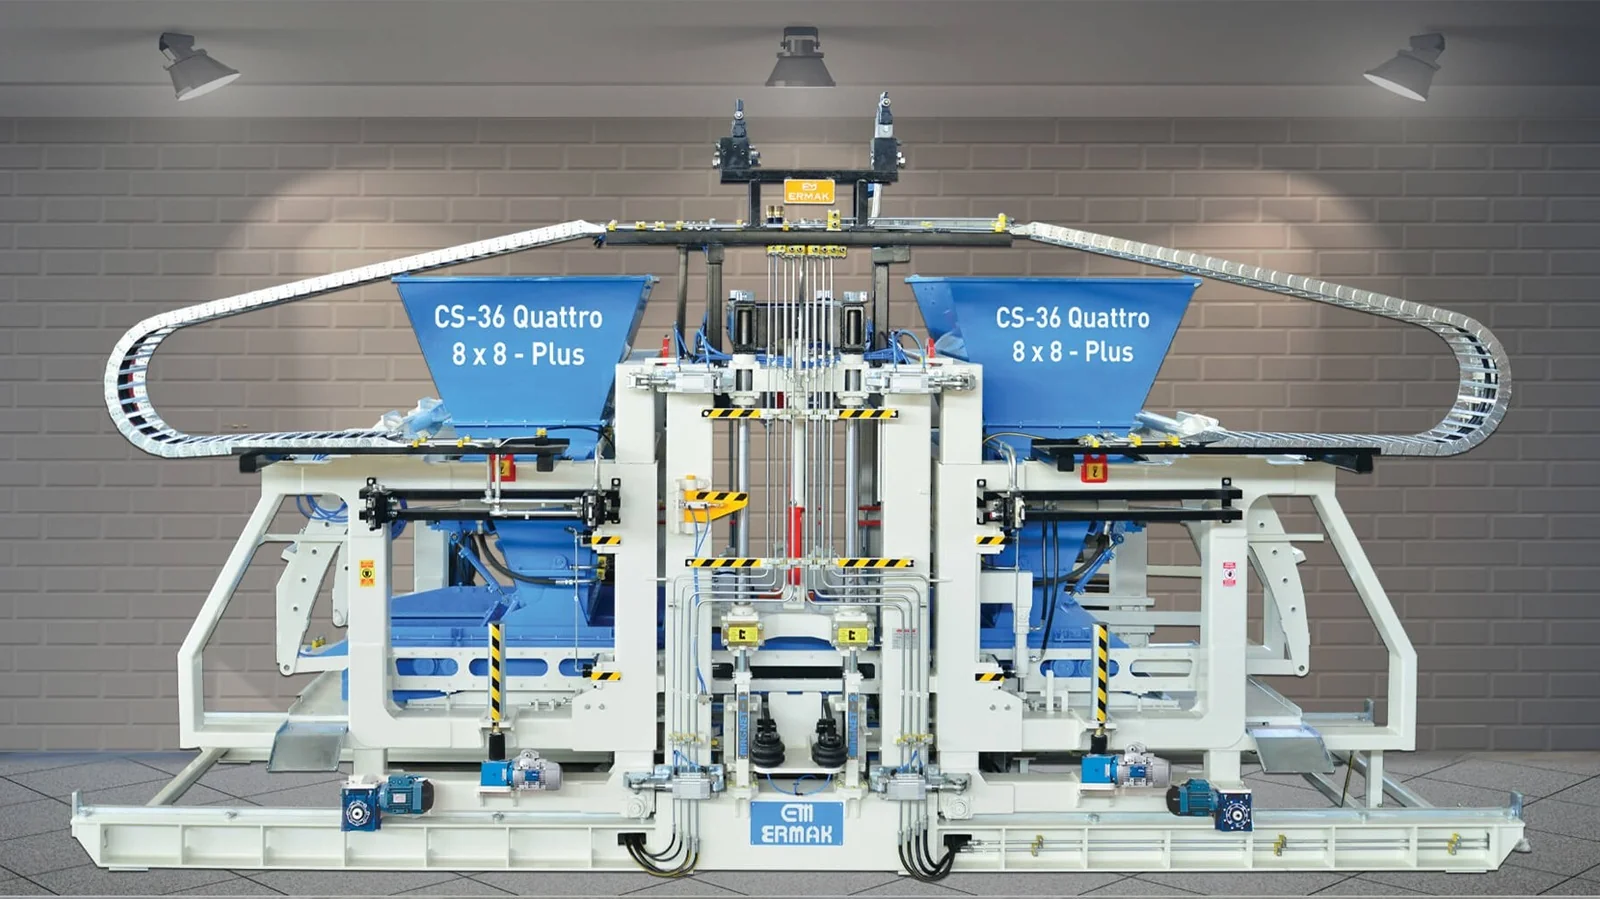
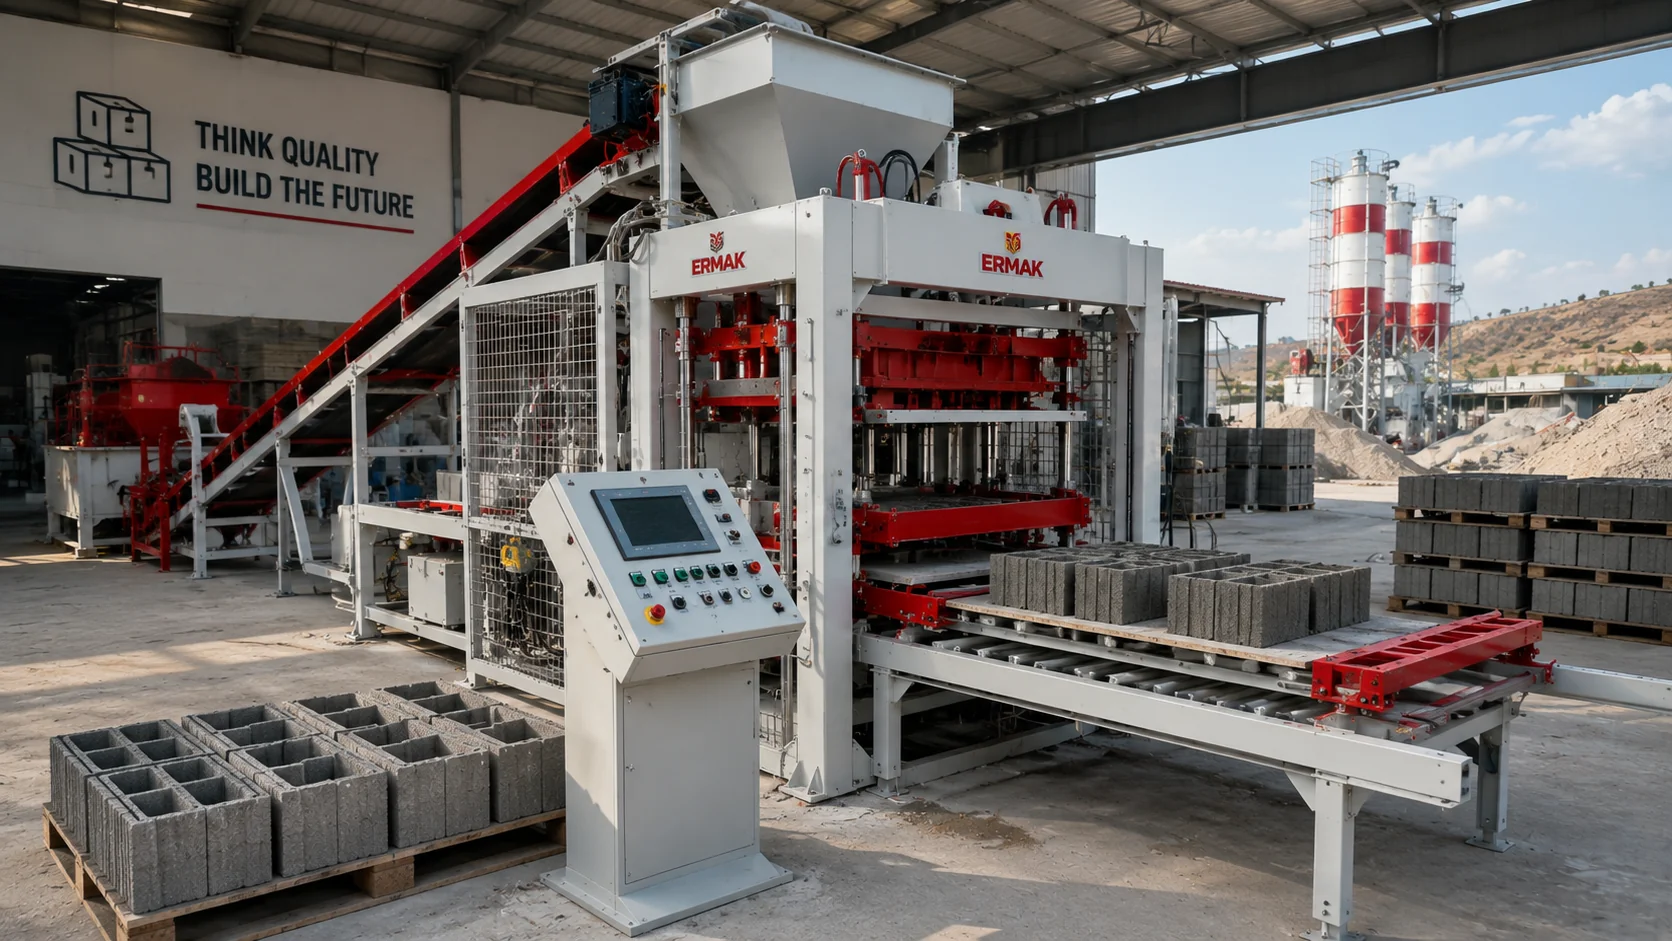
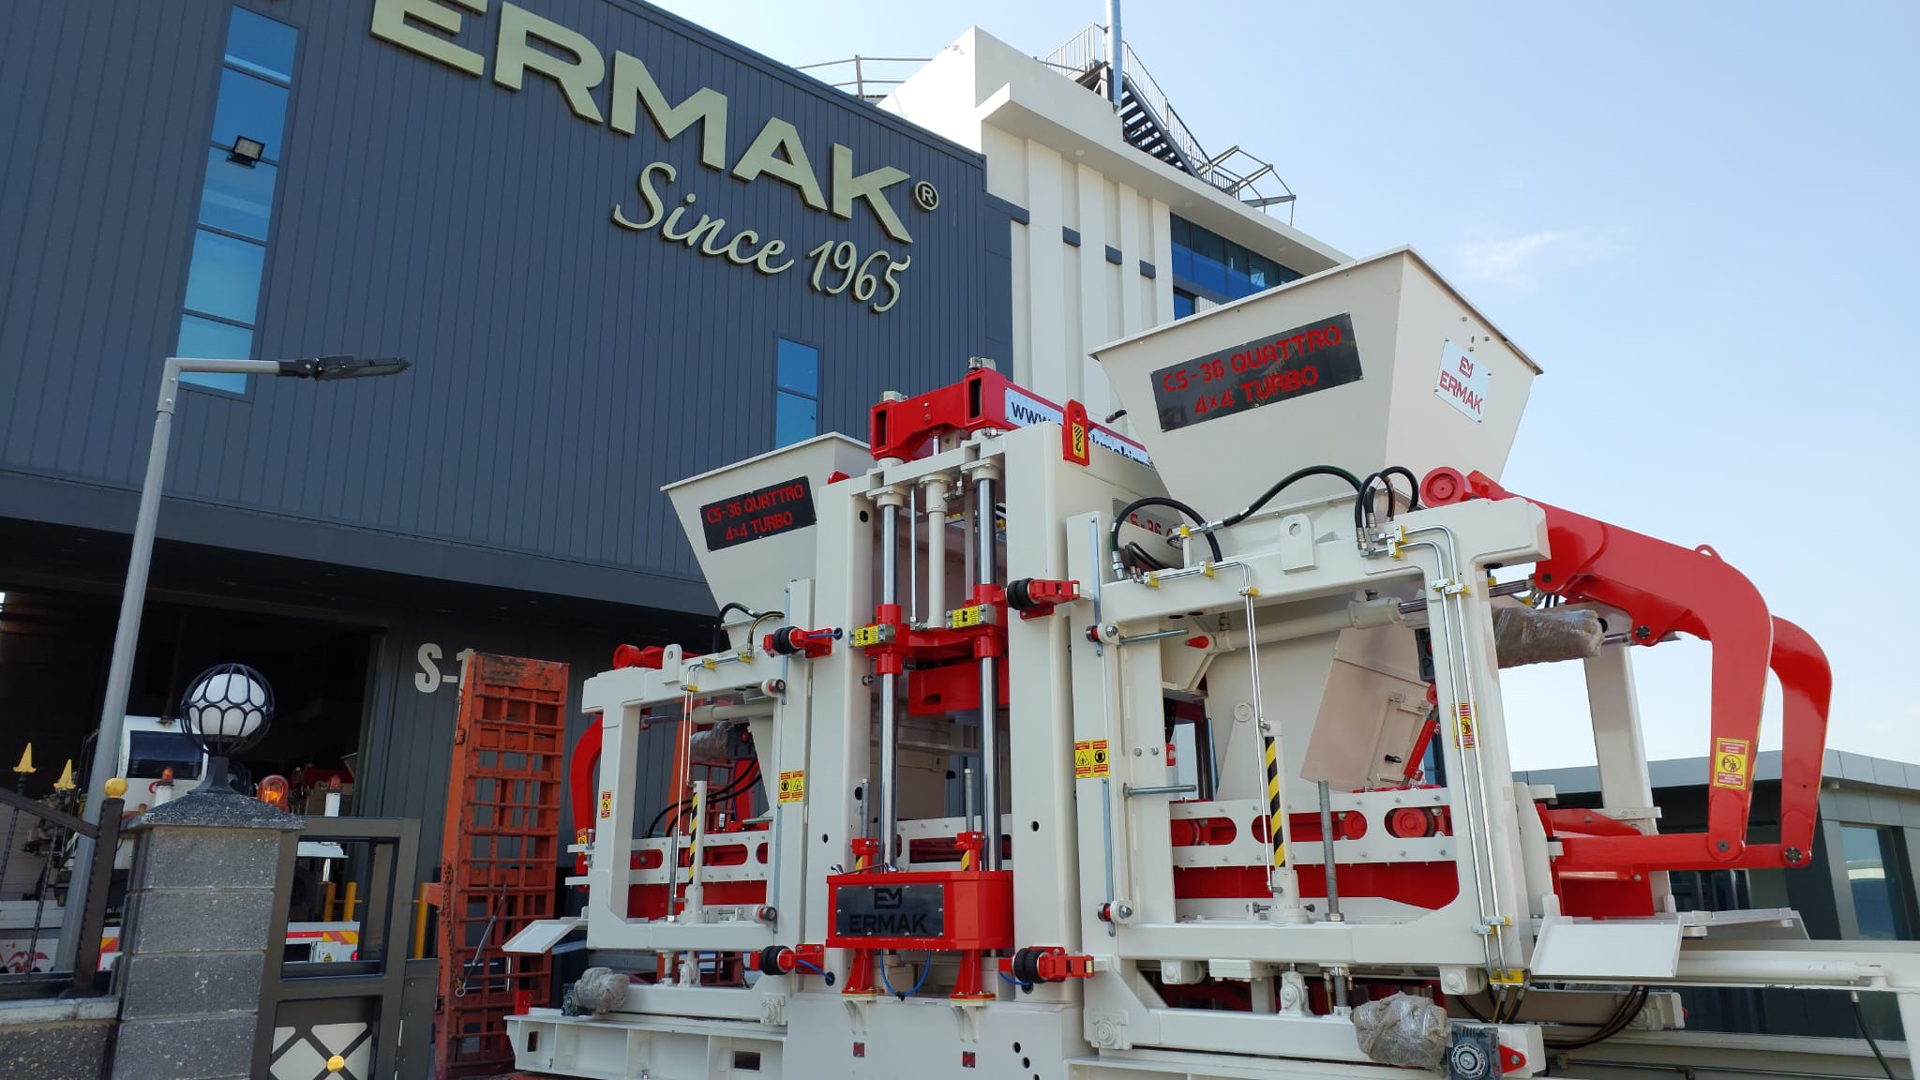
Ermak’s current product range demonstrates how capacity varies significantly by machine class. For standard 20 × 40 × 20 cm blocks, the CS-25 Power Plus is currently listed at approximately 10,000–12,000 pieces per eight hours, while the CS-36 Quattro 8X8 Plus is listed at 16,000–20,000 and the CS-42 Quattro 8X8 Plus at 25,000–30,000 pieces per eight hours.

So how should concrete block machine production capacity actually be calculated?

What Does Concrete Block Machine Capacity Mean?

Concrete block machine capacity describes the quantity of a specific product that can be manufactured during a defined period.

For hollow blocks and similar products, capacity is commonly expressed as:

  • Pieces per hour
  • Pieces per shift
  • Pieces per eight hours
  • Pieces per day

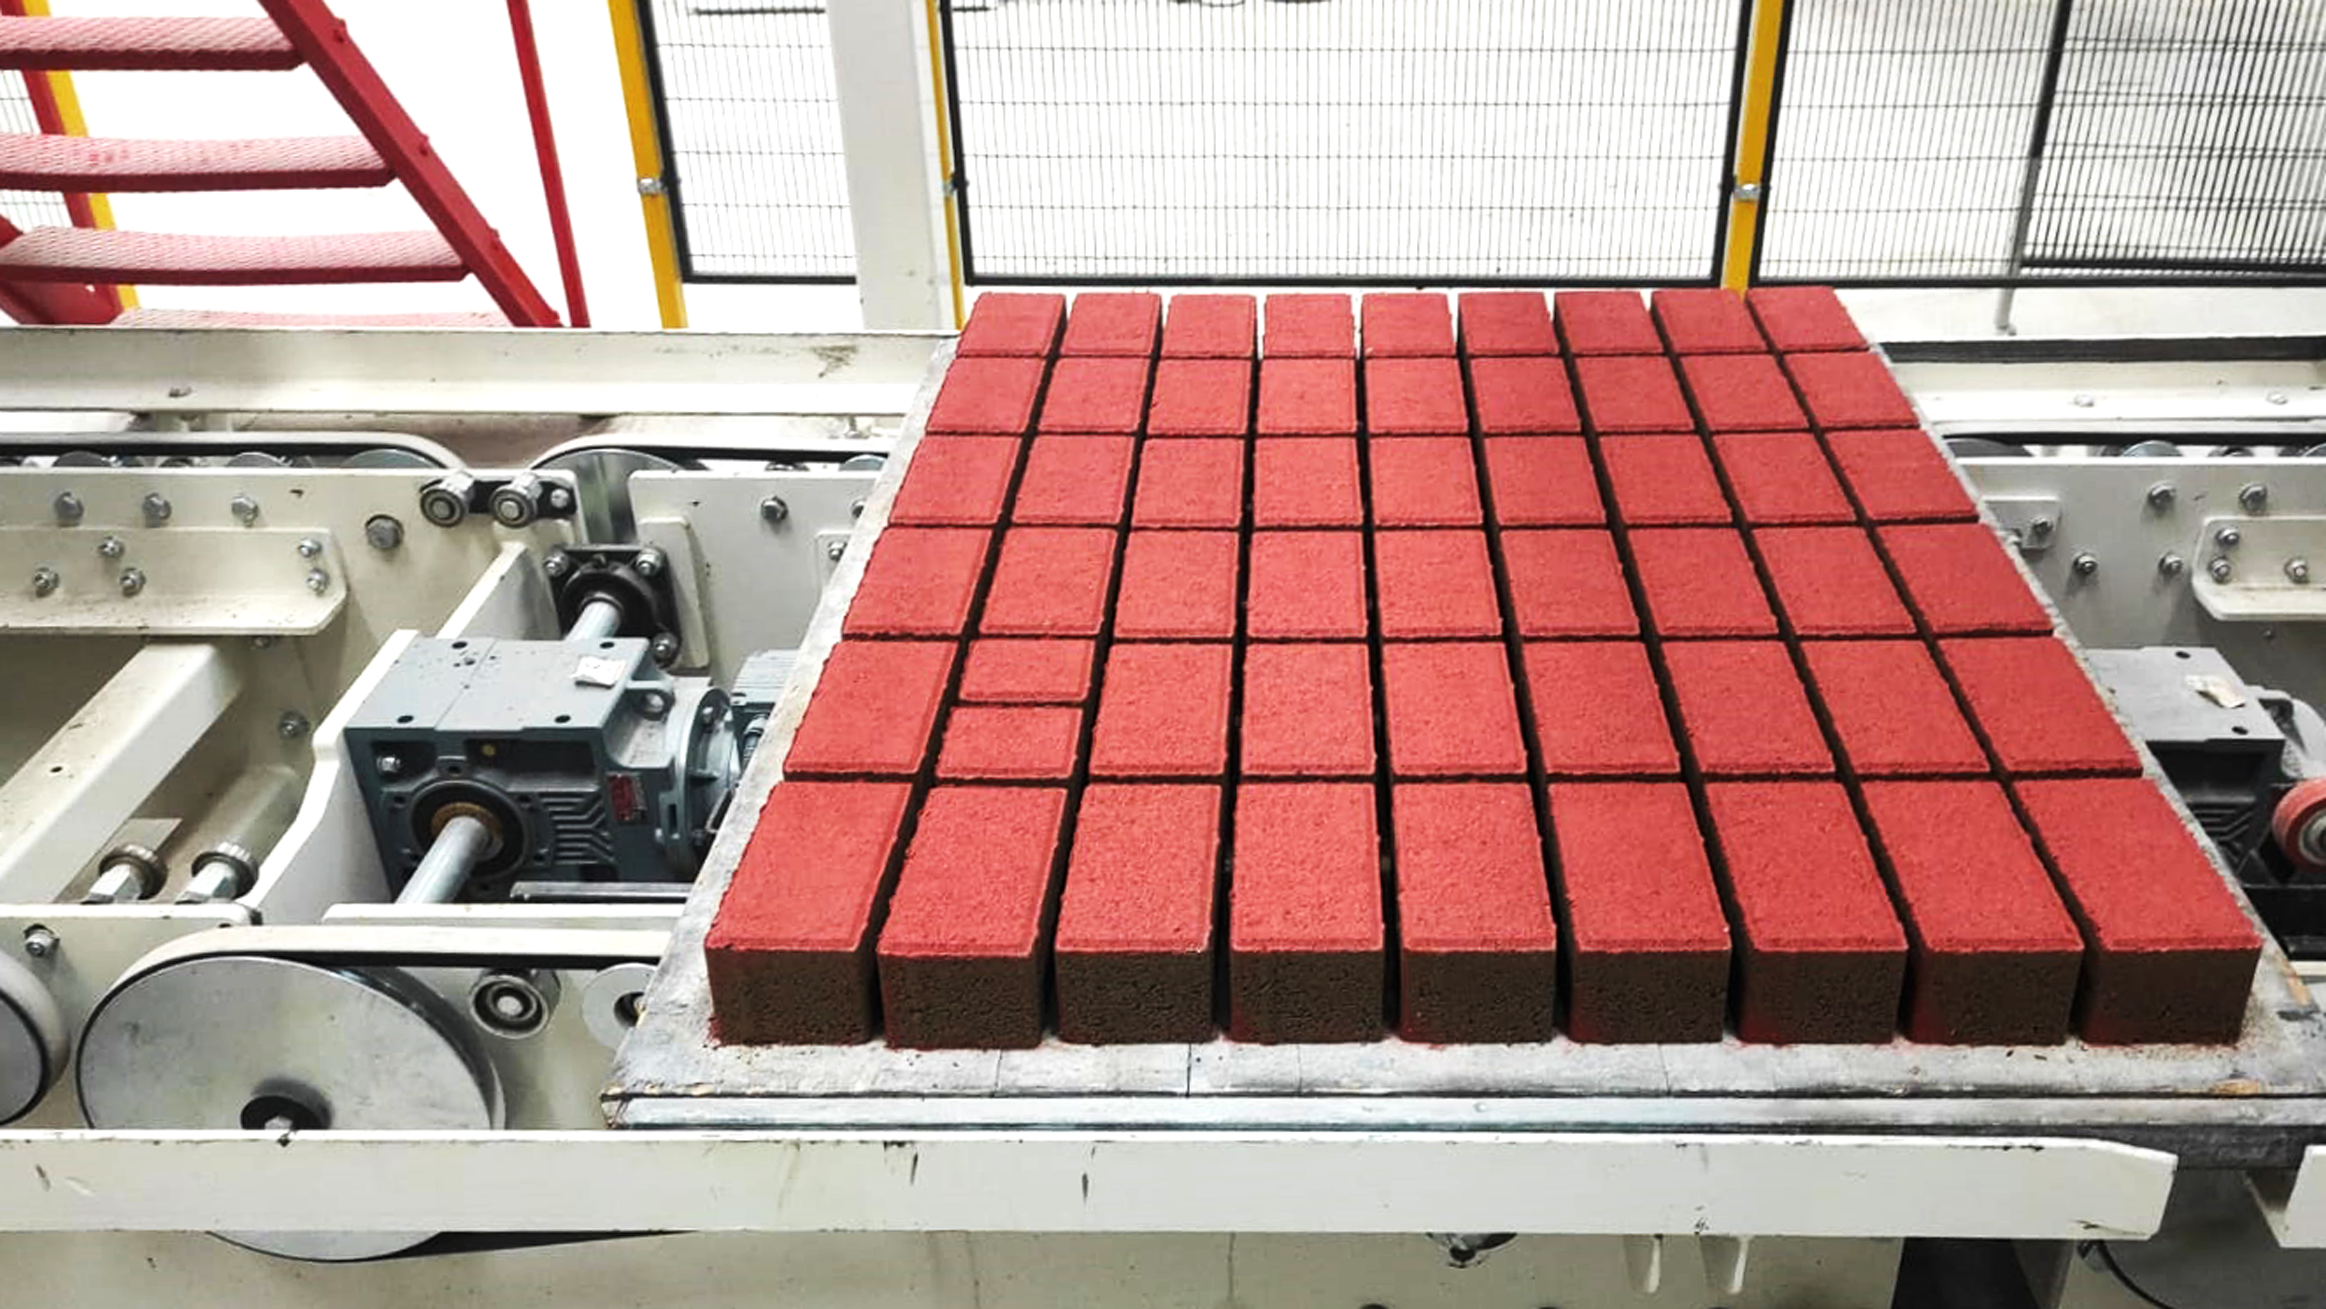
For paving stones, output is often expressed as:

  • m² per hour
  • m² per shift
  • m² per eight hours

This distinction is important.

A statement such as:

“The machine produces 25,000 pieces per shift.”

has limited value unless the supplier also specifies:

  • Which product?
  • What dimensions?
  • How many products per mould?
  • What cycle time?
  • What pallet size?
  • How long is the shift?
  • Is the figure theoretical or practical?

Ermak’s CS-42 Quattro 8X8 Plus, for example, is currently listed at 25,000–30,000 standard 20 × 40 × 20 cm blocks per eight hours and 1,500–1,800 m² of pavers per eight hours. The same machine uses a 1350 × 1400 mm-class production pallet.

This immediately shows why capacity must always be connected to a defined product.

The Basic Concrete Block Capacity Formula

The simplest theoretical calculation requires two main figures:

  1. Number of products produced per cycle
  2. Machine cycle time

The basic formula is:

Hourly theoretical capacity = Products per cycle × Cycles per hour

Cycles per hour can be calculated as:

3,600 seconds ÷ Cycle time in seconds

For example, assume that a machine:

  • Produces 18 blocks per cycle
  • Has an 18-second cycle time

Theoretical cycles per hour:

3,600 ÷ 18 = 200 cycles/hour

Theoretical hourly output:

200 × 18 = 3,600 blocks/hour

For an eight-hour shift:

3,600 × 8 = 28,800 blocks

So the theoretical production capacity is:

28,800 blocks per eight hours

But this does not necessarily mean that the factory will ship 28,800 saleable blocks at the end of every shift.

That is where real capacity calculation begins.

Why Theoretical and Actual Capacity Are Different

A concrete block factory does not normally operate for eight hours without interruption.

Real production includes:

  • Start-up procedures
  • Machine inspection
  • Concrete plant preparation
  • Product changes
  • Mould changes
  • Cleaning
  • Maintenance
  • Material replenishment
  • Quality checks
  • Operator breaks
  • Minor adjustments
  • Unplanned stoppages

Assume the theoretical capacity is 28,800 blocks per shift.

If actual operating efficiency is 82%:

28,800 × 0.82 = 23,616 blocks

Now assume that 2% of the products are rejected during quality control:

23,616 × 0.98 = 23,144 saleable blocks

Theoretical production was:

28,800

but saleable production is approximately:

23,144

That difference can have a major impact on:

  • Annual revenue
  • Raw material requirements
  • Production cost
  • Delivery planning
  • Investment payback

This is why feasibility studies should not simply multiply catalogue capacity by annual working days.

A Better Capacity Formula

A more realistic formula can be written as:

Net saleable capacity = Theoretical capacity × Availability × Performance × Quality rate

This follows the general logic of Overall Equipment Effectiveness — OEE.

For example:

  • Theoretical output: 28,800
  • Availability: 90%
  • Performance: 95%
  • Quality rate: 98%

Calculation:

28,800 × 0.90 × 0.95 × 0.98

approximately equals:

24,130 saleable blocks

This calculation is far more useful for production planning than theoretical maximum output alone.

1. Cycle Time Is One of the Most Important Capacity Variables

A production cycle includes more than vibration.

Depending on the machine design, one cycle may involve:

  1. Production pallet entering the machine
  2. Mould positioning
  3. Concrete feeding
  4. Filling-box movement
  5. Vibration
  6. Compaction
  7. Tamper-head movement
  8. Mould lifting
  9. Fresh product leaving the machine
  10. New pallet entering

Even a small difference in cycle time can produce a large difference over a complete shift.

Assume both machines use a 12-cavity mould.

15-second cycle

3,600 ÷ 15 = 240 cycles/hour

240 × 12 = 2,880 blocks/hour

18-second cycle

3,600 ÷ 18 = 200 cycles/hour

200 × 12 = 2,400 blocks/hour

Difference:

480 blocks/hour

Over eight theoretical hours:

480 × 8 = 3,840 blocks

A difference of only three seconds per cycle can therefore represent thousands of products per shift.

2. But the Fastest Cycle Is Not Always the Best Cycle

A machine should not be evaluated according to cycle time alone.

Reducing cycle time may require shortening:

  • Concrete feeding
  • Vibration
  • Compaction

If these stages become too short, product quality may deteriorate.

This can increase:

  • Surface defects
  • Edge breakage
  • Density variation
  • Reject rate

For example:

Machine setting A

  • Cycle: 15 seconds
  • Theoretical production: 30,000 blocks
  • Reject rate: 7%

Saleable output:

27,900 blocks

Machine setting B

  • Cycle: 17 seconds
  • Production: 27,000 blocks
  • Reject rate: 1%

Saleable output:

26,730 blocks

The faster setting still wins in this simplified example, but the difference is much smaller than theoretical figures suggest.

Now include cement consumption, customer complaints, packaging losses and maintenance load, and the economic result may change again.

Therefore the correct objective is:

The highest sustainable saleable output, not simply the shortest possible cycle.

3. Mould Cavity Count Has a Direct Effect on Capacity

Two machines operating at the same cycle time can have completely different production capacities if their mould sizes differ.

Suppose:

Machine A

  • 12 blocks per cycle
  • 18 seconds per cycle

Output:

2,400 blocks/hour

Machine B

  • 18 blocks per cycle
  • 18 seconds per cycle

Output:

3,600 blocks/hour

The cycle time is identical.

The difference comes from the number of products that fit into one mould cycle.

Ermak’s current CS-36 Quattro 8X8 Plus is described as a 12-block configuration, while the CS-42 Quattro 8X8 Plus is described as an 18-block configuration. Their published standard block capacities are respectively 16,000–20,000 and 25,000–30,000 pieces per eight hours.

This is why asking only for cycle time can produce a misleading comparison.

4. Production Pallet Size Influences Mould Capacity

The production pallet defines the available working area below the mould.

A larger pallet can allow more product cavities per cycle, depending on product dimensions and mould design.

Ermak’s current product range provides a useful example:

Machine Production Pallet Standard 20 × 40 × 20 Block Capacity
CS-25 Power Plus 950 × 1300 mm 10,000–12,000 pcs/8 h
CS-36 Quattro 8X8 Plus 1150 × 1400 mm 16,000–20,000 pcs/8 h
CS-42 Quattro 8X8 Plus 1350 × 1400 mm 25,000–30,000 pcs/8 h

These values are currently listed in Ermak’s English product portfolio.

However, a larger pallet does not automatically guarantee better production economics.

Larger systems can require:

  • Larger moulds
  • More concrete per cycle
  • More powerful vibration
  • Larger curing racks
  • Larger handling equipment
  • More production pallets

Pallet size should therefore be considered as part of the complete plant design.

5. Product Dimensions Change Capacity

A machine does not produce every concrete product at the same rate.

Product dimensions affect:

  • Number of cavities
  • Concrete volume per cycle
  • Feeding time
  • Vibration time
  • Product height
  • Mould geometry

A 20 × 40 × 20 cm hollow block and a small paving stone cannot be compared using the same “pieces per hour” figure.

This is one reason paver capacity is often stated in square metres rather than pieces.

A machine may manufacture hundreds of small pavers per hour but fewer large blocks.

Therefore capacity comparison must always use the same product.

6. Product Height Can Affect Cycle Time

Taller products generally require more concrete and may require different:

  • Feeding times
  • Vibration settings
  • Mould movements
  • Compaction parameters

Ermak’s CS-42 Quattro 8X8 Plus is currently specified for block production heights of 40–400 mm, while another CS-42 product description notes the ability to manufacture various products within a wider overall product range.

The important point is that a machine’s minimum and maximum production height do not mean every height will be produced at the same cycle time.

7. Concrete Feeding Time Can Become a Bottleneck

Before compaction begins, the mould must receive enough concrete.

If the feeding system is slow:

  • The cycle becomes longer.
  • Capacity falls.

If feeding is too fast but uneven:

  • Some cavities may contain too much concrete.
  • Others may be underfilled.

This can create differences in:

  • Product weight
  • Product height
  • Density

The feeding system therefore has to balance speed and uniformity.

This is especially important on large moulds where concrete must spread across a wide pallet area.

8. Vibration Time Must Be Included in Capacity Calculations

Vibration is part of the production cycle.

Its purpose is to compact relatively dry concrete inside the mould.

Shorter vibration can reduce cycle time, but insufficient vibration can increase rejects.

Longer vibration can improve compaction up to a point, but unnecessary vibration can:

  • Extend the cycle
  • Reduce hourly output
  • Increase mechanical loading

Ermak’s Quattro 8X8 Plus uses its VIBRO-180 system, which the company currently specifies at 180 kN vibration force with automatic lubrication.

For production-capacity calculations, vibration should therefore be viewed not as an isolated technical specification but as part of the total effective cycle.

9. Mould Change Time Can Significantly Reduce Shift Capacity

A factory manufacturing only one product all day may achieve a very different net capacity from a factory changing products several times per shift.

Every mould change can require:

  • Machine stoppage
  • Removal of the previous mould
  • Installation of the new mould
  • Tamper-head setup
  • Parameter adjustment
  • Trial production

Ermak states that the automatic mould-change system used on certain Quattro machines can allow production with the new mould to begin within a maximum of approximately 15 minutes under the stated conditions.

Why does this matter?

Assume an older process takes 60 minutes per mould change.

A faster system takes 15 minutes.

Time saved:

45 minutes per change

If a factory performs 20 changes per month:

45 × 20 = 900 minutes

or:

15 production hours

Those 15 hours can translate into a significant amount of annual output.

10. Product Change Frequency Should Be Included in Capacity Planning

Even without changing the mould, changing products can require:

  • Recipe changes
  • Face-mix changes
  • Pigment cleaning
  • Machine adjustments
  • Quality checks

For example, a paver plant producing:

  • Grey pavers in the morning
  • Red pavers at noon
  • Black pavers in the afternoon

may lose considerably more production time than a factory producing one long batch.

This is why plant managers should distinguish between:

Machine capacity

and:

Production-schedule capacity.

The more fragmented the production schedule, the lower net output may become.

11. Batch Plant Capacity Must Match Machine Demand

A concrete block machine cannot produce without concrete.

If the main machine requires more concrete than the batching plant can provide, the machine waits.

Assume:

  • Block machine demand: 25 m³/hour
  • Batching plant output: 19 m³/hour

The complete line cannot sustainably operate at 25 m³/hour equivalent production.

Its material supply is limited to approximately 19 m³/hour.

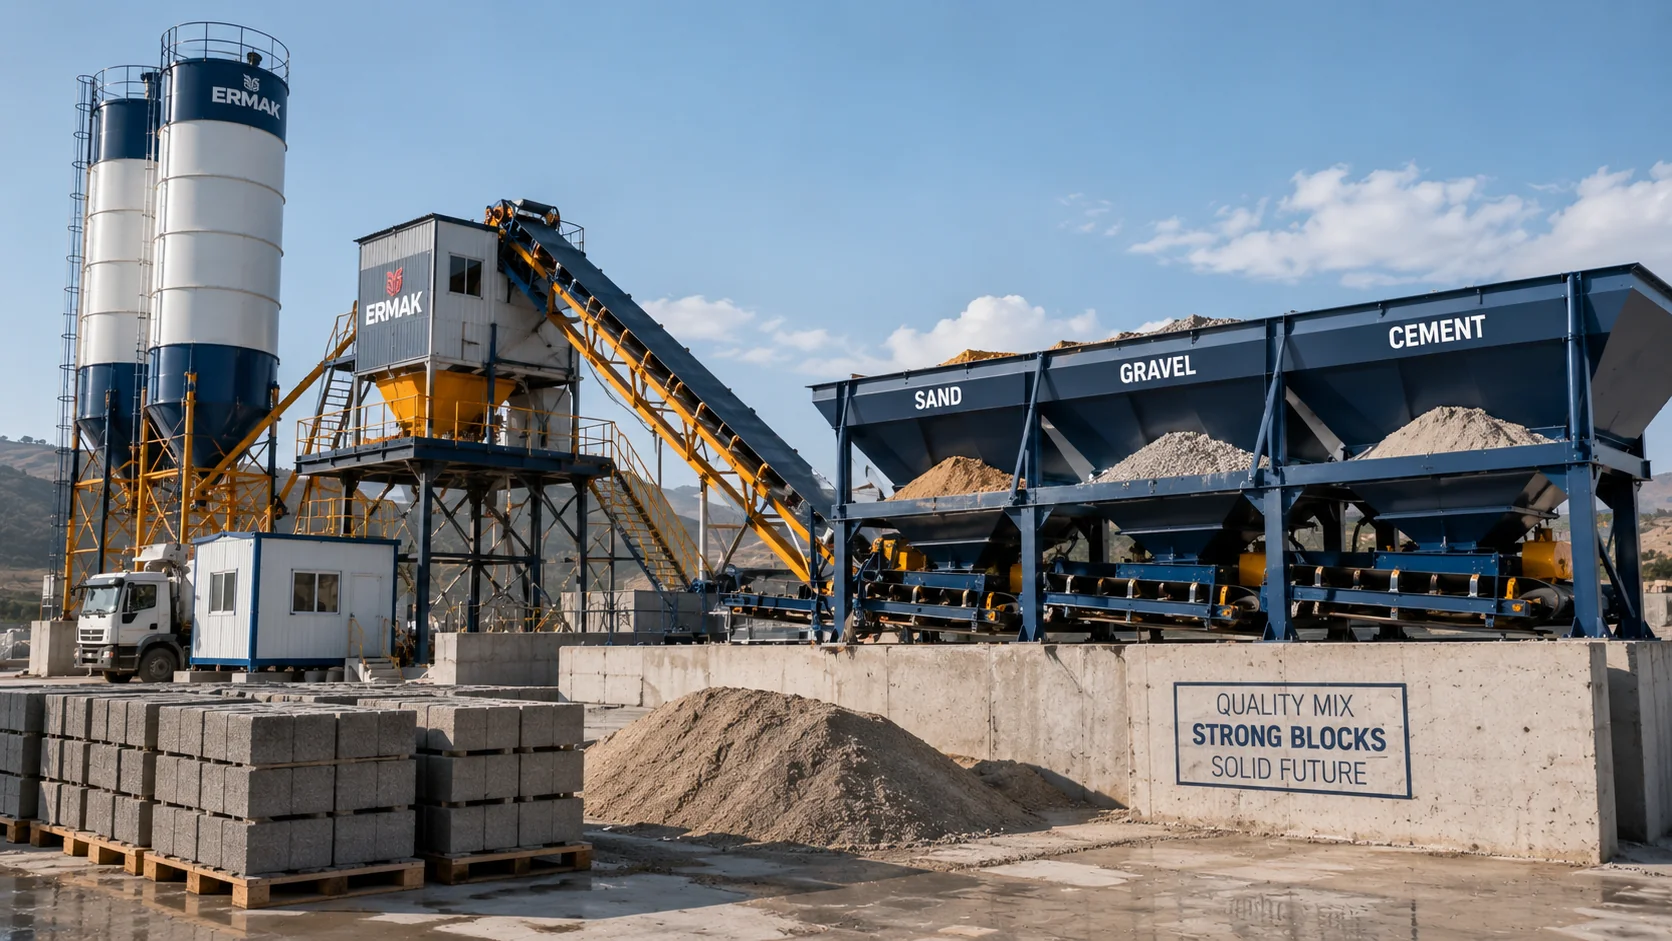
Ermak’s existing turnkey plant guidance makes the same point: batching, mixing, block production, curing and packaging should all be planned around compatible capacities.

This is one of the most important rules in plant engineering:

The slowest critical process sets the sustainable plant capacity.

12. Mixer Capacity Must Be Calculated from Complete Batch Time

Mixer capacity should not be calculated from nominal volume alone.

Assume a mixer produces:

  • 1.0 m³ net concrete per batch

and the complete batch cycle includes:

  • Aggregate loading
  • Cement loading
  • Water dosing
  • Mixing
  • Discharge

with a total time of 120 seconds.

Cycles per hour:

3,600 ÷ 120 = 30

Net hourly output:

30 × 1 = 30 m³/hour

Now assume the same mixer takes 150 seconds because loading and discharge are slow:

3,600 ÷ 150 = 24 batches/hour

Net capacity becomes:

24 m³/hour

The mixer nameplate did not change.

The real hourly output did.

This illustrates why machine and mixer cycle studies must be performed together.

13. Double-Layer Paver Production Can Change Capacity

Double-layer paving-stone production typically requires:

  • Base concrete
  • Face concrete

and potentially:

  • Two mixers
  • Additional aggregate handling
  • Pigment dosing
  • Additional feeding operations

This can change the production cycle and material flow.

A machine that can achieve a certain output in single-layer block production may operate differently when producing coloured double-layer paving stones.

Product-specific capacity should therefore always be requested.

14. Production Pallet Availability Can Limit the Machine

Production pallets circulate through the plant:

Block machine → Wet side → Curing → Dry side → Packaging → Pallet return → Block machine

If the plant does not have enough pallets, the machine can run out of empty pallets even when all equipment is mechanically functioning.

Required pallet quantity depends on:

  • Pallets per hour
  • Curing duration
  • Handling time
  • Number of shifts
  • Pallet return time
  • Spare-pallet allowance

For example, if:

  • Machine output = 120 pallets/hour
  • Pallet circulation time = 10 hours

a simplified minimum circulation requirement is:

120 × 10 = 1,200 pallets

Additional reserve may also be needed.

A shortage of production pallets can therefore become a capacity bottleneck.

15. Curing Capacity Must Match Pallet Production

Fresh concrete products require curing.

If the block machine produces:

120 pallets/hour

but the curing system can accept only:

90 pallets/hour

the production line will eventually stop.

It does not matter that the machine itself can mechanically continue at 120 pallets/hour.

The plant has nowhere to put the products.

Ermak’s turnkey plant guidance explicitly treats curing capacity as one of the systems that must be matched to the main machine.

This is why complete plant capacity should never be calculated from the block machine alone.

16. Dry-Side Capacity Matters Too

After curing, the products must leave the curing system.

The dry side can include:

  • Lowerator
  • Product conveyor
  • Cubing
  • Commercial pallet transfer
  • Packaging
  • Empty production-pallet return

If the dry side operates more slowly than the wet side, cured products accumulate.

Eventually:

  • Production pallets are not returned quickly enough.
  • Curing space remains occupied.
  • The block machine slows or stops.

This is another example of a downstream system controlling upstream capacity.

17. Packaging Capacity Must Be Included

Imagine that the block machine produces:

25,000 blocks per shift

but the packaging line can handle only:

18,000 blocks per shift.

The factory cannot sustainably dispatch 25,000 blocks every shift.

Finished products will accumulate.

This is why turnkey plant design should include:

  • Cubing capacity
  • Packaging rate
  • Pallet availability
  • Forklift logistics
  • Finished-product storage

Ermak’s existing turnkey plant article similarly emphasizes that packaging should be treated as part of overall plant capacity rather than as an afterthought.

18. Forklift and Logistics Capacity Can Become a Hidden Bottleneck

Even if the machines are correctly balanced, internal logistics can limit output.

Examples include:

  • Insufficient forklifts
  • Narrow factory aisles
  • Congested storage areas
  • Poor pallet flow
  • Slow truck loading

A fully automated block machine may sit idle because the finished-product area is full.

This is not a machine-capacity problem.

It is a factory-flow problem.

19. Availability Should Be Included in Net Capacity

Availability measures how much of scheduled production time the machine is actually available.

If an eight-hour shift contains:

  • 30 minutes planned maintenance
  • 20 minutes cleaning
  • 15 minutes adjustment
  • 25 minutes unexpected stoppage

Total lost time:

90 minutes

Actual available production time:

480 – 90 = 390 minutes

Availability:

390 ÷ 480 = 81.25%

Even if the machine performs perfectly while running, net output is reduced by the time it is unavailable.

20. Performance Losses Matter Even When the Machine Is Running

A machine may technically be running but not at its ideal rate.

Examples:

  • Slow concrete feeding
  • Operator delays
  • Poor pallet movement
  • Conservative vibration settings
  • Material variability

Assume ideal cycle time is 15 seconds.

Real average cycle time is 17 seconds.

The machine is not “stopped,” but performance is lower.

This difference should be included in realistic capacity studies.

21. Reject Rate Must Be Subtracted

Suppose a factory produces:

20,000 blocks

but:

600 blocks

are rejected.

Saleable production:

19,400 blocks

Reject rate:

3%

If investors calculate revenue using 20,000 blocks, the production model is overstated.

The relevant capacity for business planning is:

saleable products, not total moulding cycles.

22. Example: Full Net Capacity Calculation

Assume a machine has:

  • 18 blocks per cycle
  • 18-second theoretical cycle
  • 8-hour shift

Step 1 — Theoretical cycles per hour

3,600 ÷ 18 = 200 cycles

Step 2 — Theoretical output per hour

200 × 18 = 3,600 blocks

Step 3 — Theoretical shift capacity

3,600 × 8 = 28,800 blocks

Now apply:

  • Availability: 90%
  • Performance: 96%
  • Quality rate: 98%

Step 4 — Net saleable production

28,800 × 0.90 × 0.96 × 0.98

approximately equals:

24,385 blocks per shift

Theoretical capacity:

28,800

Estimated saleable capacity:

approximately 24,400

That difference is substantial.

23. Monthly Production Capacity Calculation

Once net shift capacity is known, monthly capacity becomes easier to estimate.

Assume:

  • Net shift capacity: 20,000 blocks
  • 1 shift/day
  • 26 working days/month

Monthly production:

20,000 × 26 = 520,000 blocks

For two shifts:

20,000 × 2 × 26 = 1,040,000 blocks

However, simply adding a second shift does not always double output exactly.

Additional operating hours can increase:

  • Maintenance requirements
  • Mould wear
  • Pallet circulation requirements
  • Material logistics
  • Staffing complexity

The supporting systems must be capable of operating across the longer schedule.

24. Annual Production Capacity Calculation

Annual capacity should use realistic working days.

For example:

  • Net capacity: 20,000 blocks/shift
  • 1 shift/day
  • 300 production days/year

Annual output:

20,000 × 300 = 6,000,000 blocks/year

With two shifts:

12,000,000 blocks/year

in simplified terms.

However, annual planning should allow for:

  • Major maintenance
  • Public holidays
  • Seasonal shutdowns
  • Market fluctuations
  • Mould changes

A 365-day theoretical calculation is rarely useful for normal investment planning unless the plant genuinely intends to operate continuously.

25. How to Calculate Paver Production Capacity

Paver output is usually more useful when expressed in square metres.

The basic formula is:

Area produced per cycle × Cycles per hour

Suppose one production pallet produces:

1.0 m²

of finished paving area per cycle.

Cycle time:

20 seconds

Cycles per hour:

3,600 ÷ 20 = 180 cycles

Theoretical output:

180 m²/hour

Eight-hour theoretical output:

1,440 m²

Real net output should again be adjusted for:

  • Availability
  • Performance
  • Rejects
  • Product changes

Ermak currently lists the CS-36 Quattro 8X8 Plus at 1,400–1,600 m² of pavers per eight hours and the CS-42 at 1,500–1,800 m² per eight hours under their stated production conditions.

26. Do Not Compare Paver Capacity and Block Capacity Directly

A machine might be advertised as:

  • 25,000 blocks/shift
  • 1,800 m² pavers/shift

These figures describe different products using different units.

Neither number alone tells you that one product is produced “faster.”

The correct comparison depends on:

  • Market selling price
  • Concrete consumption
  • Mould cavities
  • Production cycle
  • Product demand
  • Margin per unit

Capacity must always be interpreted within the business model.

27. Theoretical Cycle Time Should Be Verified in Production

A supplier may provide a minimum mechanical cycle time.

Investors should ask whether this figure represents:

  • Empty machine movement
  • Test production
  • Real product production
  • Continuous eight-hour operation

A 12-second mechanical cycle shown during a demonstration may not necessarily equal a sustainable 12-second production cycle with:

  • Real concrete
  • Full mould filling
  • Required compaction
  • Commercial quality

Reference plants are valuable because they show long-term production performance rather than only demonstration speed.

28. Product Quality and Capacity Should Be Measured Together

A production report should ideally contain both:

Output

and:

Quality

For example:

Shift Total Produced Rejects Saleable Output
Shift 1 20,000 300 19,700
Shift 2 21,000 1,200 19,800

Shift 2 technically produced more products.

But saleable output increased by only:

100 blocks

while rejects increased significantly.

This example shows why production management should not reward cycle count alone.

29. Capacity per Labour Hour Can Also Be Useful

Another useful KPI is:

Saleable blocks ÷ Total labour hours

For example:

Plant A

  • 20,000 saleable blocks
  • 10 workers × 8 hours = 80 labour hours

250 blocks/labour hour

Plant B

  • 25,000 saleable blocks
  • 5 workers × 8 hours = 40 labour hours

625 blocks/labour hour

This metric can be particularly useful when comparing different automation levels.

30. Energy per Product Should Be Considered Together with Capacity

A higher-capacity machine may use more electricity in total.

However, it may use less energy per product.

For example:

Machine A

  • 700 kWh/shift
  • 10,000 saleable blocks

70 kWh / 1,000 blocks

Machine B

  • 1,200 kWh/shift
  • 20,000 saleable blocks

60 kWh / 1,000 blocks

Machine B consumes more electricity overall but less per saleable block.

Capacity, energy and product quality should therefore be analysed together.

31. Future Demand Should Influence Capacity Selection

Investors should not select equipment only for today’s production.

However, purchasing an extremely oversized machine “just in case” can also be expensive.

A better approach is:

Current demand + realistic growth margin

For example, if current profitable demand is:

10,000 blocks/day

and the three-year target is:

14,000 blocks/day

a machine with some reserve capacity may make sense.

A system designed for 30,000 blocks/day may require:

  • Higher capital expenditure
  • Larger batching plant
  • More curing capacity
  • Larger electrical infrastructure
  • More pallets
  • Larger storage areas

without generating additional revenue.

Unused capacity is still paid-for capacity.

32. The Complete Plant Should Be Balanced

A useful plant capacity table might look like this:

Process Sustainable Capacity
Batching plant 28,000 blocks/day equivalent
Mixer 27,000 blocks/day equivalent
Block machine 25,000 blocks/day
Curing system 23,000 blocks/day
Packaging 20,000 blocks/day

What is the sustainable plant capacity?

Not 28,000.

Not 25,000.

Approximately:

20,000 blocks/day

because packaging is the bottleneck.

Ermak’s turnkey plant guidance makes the same broader point: batching, mixing, block production, curing and packaging must be balanced if the factory is expected to operate as one complete production system.

33. How Ermak Capacity Classes Compare

Ermak’s current English product portfolio includes several capacity classes.

CS-25 Power Plus

Current published figures include:

  • 10,000–12,000 standard blocks/8 hours
  • 950 × 1300 mm pallet

CS-36 Quattro 8X8 Plus

Current published figures include:

  • 16,000–20,000 standard 20 × 40 × 20 cm blocks/8 hours
  • 1,400–1,600 m² pavers/8 hours
  • 1150 × 1400 mm-class pallet
  • 40–400 mm block production height

CS-42 Quattro 8X8 Plus

Current published figures include:

  • 25,000–30,000 standard 20 × 40 × 20 cm blocks/8 hours
  • 1,500–1,800 m² pavers/8 hours
  • 1350 × 1400 mm-class pallet
  • 40–400 mm block production height

These figures illustrate how production pallet size, mould configuration and machine class influence output.

They also demonstrate why the correct machine should be selected according to required plant capacity, not simply maximum available capacity.

34. Questions to Ask When Comparing Block Machine Capacity

Before accepting any production-capacity claim, ask:

  1. Which product is the capacity based on?
  2. What are the product dimensions?
  3. How many products are produced per cycle?
  4. What is the cycle time?
  5. Is this minimum or average cycle time?
  6. What pallet size is used?
  7. What is the mould cavity count?
  8. Is capacity theoretical or real?
  9. How many working hours are assumed?
  10. Are cleaning periods included?
  11. Are mould changes included?
  12. Is the batching plant included in the study?
  13. What mixer capacity is required?
  14. How many production pallets are required?
  15. What curing capacity is required?
  16. What dry-side capacity is required?
  17. What packaging capacity is required?
  18. What reject rate is assumed?
  19. How many operators are required?
  20. Can the figures be verified at an operating reference plant?

These questions turn a marketing number into a technical capacity study.

35. Common Mistakes When Calculating Concrete Block Capacity

Some of the most common errors include:

  • Using catalogue maximum as annual production
  • Ignoring product dimensions
  • Comparing different mould configurations
  • Ignoring shift losses
  • Ignoring reject rate
  • Ignoring batching capacity
  • Ignoring mixer cycle time
  • Ignoring mould changes
  • Ignoring curing capacity
  • Ignoring packaging
  • Ignoring production-pallet circulation
  • Assuming two shifts always equal exactly twice the output
  • Buying capacity far above market demand

Most of these mistakes come from treating the block machine as the entire factory.

It is not.

36. Calculate Saleable Capacity, Not Maximum Press Cycles

The most commercially meaningful production formula is not:

Maximum cycles × Products per cycle

It is closer to:

Effective cycles × Products per cycle × Quality rate

and even that figure must fit the plant’s:

  • Batching
  • Curing
  • Packaging
  • Logistics

capacity.

In other words, the goal is not to answer:

“How many times can the press move?”

The goal is to answer:

“How many products can the factory manufacture, cure, package and sell?”

Concrete Block Machine Capacity Calculation Checklist

Before finalising an investment, confirm:

  • Target product is defined.
  • Product dimensions are known.
  • Mould cavity count is confirmed.
  • Real cycle time is known.
  • Pallet size is confirmed.
  • Theoretical hourly capacity is calculated.
  • Shift availability is estimated.
  • Performance factor is estimated.
  • Reject rate is estimated.
  • Net saleable production is calculated.
  • Batching capacity is sufficient.
  • Mixer output is sufficient.
  • Production pallet quantity is sufficient.
  • Curing capacity matches production.
  • Dry-side handling matches production.
  • Packaging matches production.
  • Internal logistics are adequate.
  • Monthly and annual production are calculated.
  • Market demand supports the selected capacity.
  • Future growth has been considered.

Choosing the Right Capacity for a Concrete Block Plant

A concrete block machine should not be selected simply because it has the highest number in a brochure.

The correct capacity should match:

  • The products you intend to manufacture
  • Daily sales requirement
  • Number of shifts
  • Available factory space
  • Batching and curing infrastructure
  • Labour model
  • Automation level
  • Future expansion plans

Ermak’s current portfolio ranges from the CS-25 Power Plus at approximately 10,000–12,000 standard blocks per eight hours to higher-capacity CS-42 Quattro 8X8 Plus configurations at 25,000–30,000 standard blocks per eight hours.

The right solution is not automatically the smallest or the largest.

It is the system that can deliver the required quantity of saleable products with the best balance of:

  • Investment cost
  • Operating cost
  • Product quality
  • Production reliability
  • Future growth

A well-designed concrete block factory therefore begins with a realistic capacity study before equipment is ordered.

Because in concrete block manufacturing, machine capacity is a specification — plant capacity is a system result.

For investors planning a new concrete block, hollow-block or paving-stone production facility, Ermak can evaluate machine size, batching requirements, mould configuration and complete line capacity according to the targeted products and daily output.

Frequently Asked Questions

How is concrete block machine production capacity calculated?

The basic theoretical formula is:

Products per cycle × 3,600 ÷ Cycle time in seconds

This gives theoretical hourly production. Real production should then be adjusted for availability, performance losses and rejected products.

What is the difference between theoretical and actual capacity?

Theoretical capacity assumes continuous production under ideal conditions. Actual capacity includes cleaning, maintenance, mould changes, operator delays, material interruptions and rejects.

How many blocks can a concrete block machine produce in eight hours?

It depends on the machine and product. Ermak currently lists the CS-25 Power Plus at approximately 10,000–12,000 standard blocks per eight hours, CS-36 Quattro 8X8 Plus at 16,000–20,000 and CS-42 Quattro 8X8 Plus at 25,000–30,000 pieces under their stated conditions.

Does cycle time determine machine capacity?

It is one of the main variables, but not the only one. Mould cavity count, pallet size, product dimensions, feeding, vibration, downtime and reject rate also influence actual output.

Why does mould cavity count matter?

More cavities allow more products to be produced per machine cycle. For example, Ermak currently describes the CS-36 Quattro 8X8 Plus as a 12-block configuration and the CS-42 as an 18-block configuration.

Does production pallet size affect capacity?

Yes. A larger production pallet can allow a larger mould and more products per cycle, depending on product geometry. Ermak’s current models use different pallet sizes across different capacity classes.

Can I multiply catalogue capacity by 300 days to calculate annual production?

You can use it as a theoretical upper reference, but a realistic annual forecast should first adjust capacity for availability, operating performance, mould changes, maintenance and rejected products.

How should reject rate be included?

Multiply gross production by the saleable quality rate. For example, if output is 20,000 products and reject rate is 3%, saleable output is approximately 19,400 products.

Can the batching plant limit concrete block machine capacity?

Yes. If the batching plant and mixer cannot supply enough concrete, the block machine will wait. The complete production line should therefore be balanced around the required output.

Can curing capacity limit production?

Yes. If fresh pallets are produced faster than the curing system can accept them, production will eventually stop even if the block machine itself has more capacity.

Does packaging affect plant capacity?

Yes. A packaging line that is slower than the production line can cause finished products and production pallets to accumulate, eventually restricting the entire factory.

Does a second shift exactly double production?

Not always. Longer operation increases maintenance demand, pallet circulation, staffing requirements and material logistics. Actual output should be calculated from measured shift performance.

What is the best KPI for block machine capacity?

One of the most useful is saleable products per shift. Additional useful indicators include products per machine hour, reject rate, OEE, blocks per labour hour and energy consumption per 1,000 saleable products.

Is the highest-capacity machine always the best investment?

No. The correct machine should match realistic sales demand and the capacity of the rest of the plant. Excess capacity increases investment without necessarily increasing profit.

What is the most important rule when comparing concrete block machines?

Always compare the same product, same operating period and same production conditions. A capacity figure without product dimensions, mould configuration and cycle assumptions is incomplete.